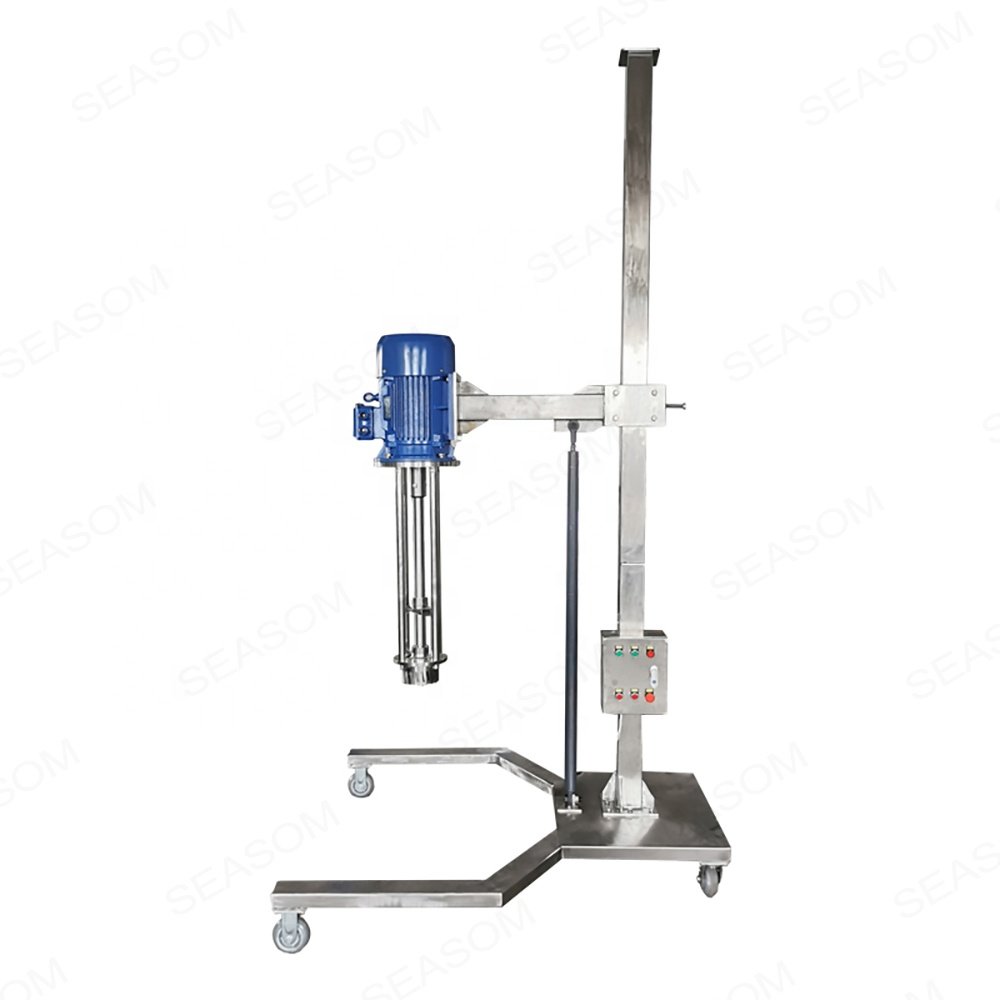
In industrial manufacturing, achieving precise formulation control, repeatable product quality, and complete ingredient blending is essential. Whether formulating pharmaceuticals, specialty chemicals, personal care products, or food and beverages, manufacturers rely on batch mixers as the core foundation of their processing lines.
Unlike continuous processing systems that blend raw materials in an uninterrupted, real-time stream, a batch mixer processes a fixed, measured volume of ingredients inside a dedicated vessel for a specified duration. This discrete processing method offers unmatched flexibility, strict recipe control, and straightforward quality assurance.
Batch Mixer Applications
Batch mixers are used in a wide variety of industrial processes.
Food and Beverage Industry
Batch mixers are commonly used for food products where recipes contain multiple ingredients that must be blended in a controlled sequence.
Typical applications include:
- Sauces
- Mayonnaise
- Ketchup
- Salad dressings
- Syrups
- Dairy products
- Fruit preparations
- Seasonings
- Food additives
For food processing, the equipment may require sanitary construction and easy cleaning.
Stainless steel such as SS304 or SS316L is commonly selected depending on the product and hygiene requirements.
Pharmaceutical Industry
Batch mixing is particularly important in pharmaceutical manufacturing because formulations often require precise ingredient ratios and controlled processing conditions.
Applications include:
- Suspensions
- Ointments
- Creams
- Gels
- Pharmaceutical solutions
- Active ingredient dispersions
Pharmaceutical batch mixers may require hygienic design, polished surfaces, sanitary connections, and controlled operating parameters.
Cosmetic Industry
Batch mixers are widely used to manufacture:
- Face creams
- Body lotions
- Shampoos
- Conditioners
- Sunscreens
- Gels
- Cosmetic emulsions
A combination of an anchor agitator and high shear homogenizer can be used when a formulation requires both bulk circulation and intensive emulsification.
Chemical Industry
Batch mixing is widely used in chemical processing because manufacturers often produce different formulations using the same equipment.
Typical applications include:
- Chemical solutions
- Pigment dispersions
- Adhesives
- Resins
- Coatings
- Polymer solutions
- Detergents
- Industrial chemicals
The mixer and wetted materials must be selected according to chemical compatibility.
Paint and Coating Industry
Batch mixers are used for blending pigments, binders, solvents, and additives.
High-speed dispersers are often used when pigment wetting and dispersion are required.
The final equipment configuration depends on:
- Pigment concentration
- Product viscosity
- Required fineness
- Batch volume
- Solvent characteristics
Water Treatment
Batch mixers can also be used in water and wastewater treatment systems.
Typical applications include:
- Coagulant preparation
- Polymer preparation
- Chemical dosing
- pH adjustment
- Flocculation
- Sludge conditioning
For water treatment, the mixer is usually selected according to tank volume, fluid viscosity, solids concentration, and required mixing intensity.
Batch mixers are deployed across virtually all processing sectors:
| Industry | Typical Applications | Primary Mixing Goal |
| Pharmaceuticals | Cough syrups, ointments, tablet granulations, suspensions | Strict cGMP compliance, sterile mixing, exact API dosing |
| Cosmetics & Personal Care | Body lotions, shampoos, hair dyes, lipsticks, mascaras | Silky texture, bubble-free de-aeration, stable emulsions |
| Food & Beverage | Mayonnaise, sauces, dairy drinks, chocolate, fruit jams | Lump-free powder hydration, oil emulsification, smooth mouthfeel |
| Chemicals & Polymers | Specialty lubricants, resins, adhesives, paints, pesticides | Uniform pigment dispersion, accelerated chemical reaction |
| Water Treatment | Coagulant preparation, Polymer preparation, Chemical dosing | Uniform dry powder blending |
Key Advantages of Batch Mixers
Choosing batch mixing over continuous inline systems delivers critical operational and economic benefits, particularly for multi-product facilities:
1. Unmatched Recipe and Dosing Precision
In batch mixing, every ingredient is pre-weighed and verified before processing begins. This eliminates flow-rate fluctuations associated with continuous dosing pumps, ensuring 100% compliance with strict formulation ratios.
2. Complete Traceability and Quality Control
If a batch fails quality control testing (e.g., pH, viscosity, or particle size distribution), only that specific, isolated batch is quarantined or discarded. In continuous mixing, an upstream dosing error can compromise hours of continuous production across multiple holding tanks.
3. Superior Versatility for Multi-Product Lines
Batch mixers are ideal for facilities producing multiple SKUs, flavors, colors, or fragrances on a single line. Changing formulations simply requires flushing or cleaning the vessel and loading new raw materials.
4. Extended Residence Time Control
Certain formulations require prolonged reaction times, heating, cooling, or vacuum de-aeration. Batch mixers allow operators to hold materials inside the vessel for as long as necessary to achieve complete hydration or chemical reaction.
5. Simple Scaling from R&D to Production
Lab-scale batch mixers share identical rotor-stator or impeller geometries with full-scale production units. Process variables like tip speed, power-to-volume ratio, and mixing time scale predictably from a 5-liter pilot vessel to a 5,000-liter production tank.
6. Handles Complex High-Viscosity Formulations
High-viscosity pastes, heavy creams, and slurries that resist continuous pumping through pipe loops can be easily managed in batch vessels equipped with bottom-discharge valves and wall-scraping agitators.

Batch Mixing vs. Continuous Mixing: A Quick Comparison
Understanding when to choose batch processing versus continuous processing depends on production volume and product variety:
| Feature / Metric | Batch Mixer | Continuous Mixer |
| Production Scale | Discrete volumes ($50\text{ L} – 10,000\text{ L}$) | High-volume, single-product ($100,000+\text{ L/day}$) |
| Flexibility | Exceptional (easy changeover for multiple SKUs) | Low (designed for dedicated, single-formula lines) |
| Ingredient Dosing | Static pre-weighing (high accuracy) | Dynamic inline flow metering (requires tight calibration) |
| Residence Time | Fully adjustable per batch | Fixed by flow rate and pipe length |
| Traceability | Isolated per batch code | Continuous lot tracking |
| Capital Investment | Lower initial equipment & piping cost | Higher initial cost for automated dosing infrastructure |

How to Select the Right Batch Mixer
To choose the optimal batch mixer for your processing plant, evaluate the following parameters:
- Batch Size and Vessel Geometry: Determine target batch volume, height-to-diameter ratio, and required head clearance for lifting stands or top-entering drives.
- Material Rheology & Viscosity: Select high-shear units for low-viscosity emulsification, or dual-shaft anchor systems for thick pastes exceeding 20,000 cPs.
- Heating / Cooling Requirements: Verify if the vessel requires an insulated steam jacket, dimple jacket, or internal heating coils.
- Vacuum and Pressure Rating: If foam or air bubbles ruin product clarity or density, select a vacuum-rated batch mixer equipped with a liquid-ring vacuum pump.
- Hygienic Standards: For food, cosmetic, or pharmaceutical uses, ensure all contact surfaces are constructed from polished 316L stainless steel with EHEDG, 3-A, or FDA sanitary compliance.
Conclusion
A batch mixer is a versatile solution for industrial processes that require controlled mixing of a predetermined quantity of material.
Its major advantages include high process flexibility, precise recipe control, wide viscosity capability, easy process optimization, and suitability for multi-ingredient formulations.
Batch mixers are widely used in food and beverage, pharmaceutical, cosmetic, chemical, paint, coating, adhesive, and water treatment industries.
The correct mixer should be selected according to the product viscosity, density, solids concentration, batch volume, mixing time, temperature, tank geometry, and required shear intensity.
For simple liquid blending, a conventional agitator may be sufficient. For demanding emulsification and dispersion processes, a high shear batch mixer or a combination of conventional agitation and high shear homogenization may provide better results.
By matching the mixer design to the actual process requirements, manufacturers can achieve more consistent product quality while controlling energy consumption, processing time, and operating costs.